If you’ve ever stepped foot in a jewelry studio, or even browsed Instagram for custom engagement rings or hand-stamped necklaces, you know this space is equal parts old-world craft and bleeding-edge innovation. Ten years ago, if a designer said they “3D printed” a wedding band, people would’ve thought they meant a plastic prototype for a sketch, not a finished piece worn daily on someone’s hand. Today? 3D printing for jewelry is the backbone of so many custom lines, small-batch brands, and even big-name houses that used to rely solely on hand-wax carving and lost-wax casting. As someone who’s been on the supplier side of this game for a while—chatting with designers, shop owners, and one-off makers every week—I’ve noticed most people get tripped up on the different types of jewelry 3D printers out there. It’s not just one generic “3D printer” for all jewelry needs—pick the wrong one, and you’ll waste thousands on materials, struggle with post-processing, and end up with a piece that looks worse than a hand-carved wax mistake. Jewelry 3D Printer
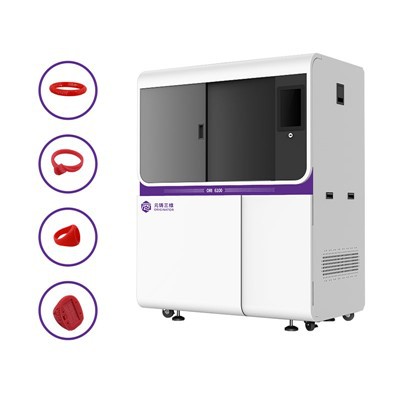
Let’s break this down like I’d break it down over a coffee with a new designer who’s just dipping their toes into this. No jargon, no fancy corporate fluff, just what actually works for who, what, and why.
First, let’s start with the OG jewelry 3D printer, the one that kicked this whole industry into high gear: Stereolithography, or SLA for short. This is the workhorse for 90% of jewelry designers, especially those making wax masters or finished casting parts. Here’s how it works, super simply: it uses a UV laser to trace tiny layers (we’re talking 25 to 100 microns thick—like a strand of human hair, basically) across a pool of liquid photopolymer resin. The laser hits the resin and instantly cures it, turning the liquid into a solid plastic layer. The bed pulls down, a new layer of resin is spread, and the laser does its thing again until your entire piece is built. For jewelry, SLA is game-changing because of the detail. Think delicate filigree on a locket, tiny micro-prong settings for a halo ring, or even the tiny engraving of a kid’s name on a band—SLA can pull that off no problem. The resin used for SLA printers here is specific, though: you don’t use the cheap Halloween costume resin. Jewelry-specific SLA resin is formulated to burn clean during the lost-wax casting process. Wait, right—most jewelry 3D prints aren’t the final metal piece; they’re the pattern you use for casting. The lost-wax method, which has been around for 6,000 years, still works like this: you melt and burn out the wax or resin master, leaving a hollow mold, then pour molten gold, silver, or platinum into that mold. SLA resin burns almost completely clean, no ash, no leftover gunk that would ruin the metal’s finish. That’s why every small jewelry shop and big brand from Tiffany to local custom designers swear by SLA. The only downside? SLA printers can be pricier for industrial models, and you have to deal with post-processing: after printing, you need to wash the part in isopropyl alcohol to get rid of excess resin, cure it under a UV light (or sunlight, if you’re desperate), then sand and polish it before casting. It’s not hard, but it’s an extra step.
Next up, something that’s been blowing up for small-batch makers and custom pieces lately: DLP, or Digital Light Processing. If you’re familiar with SLA, DLP is kind of its cheaper, faster cousin. Here’s the difference: instead of a tiny UV laser drawing each layer one line at a time, DLP uses a whole projector screen (or a digital light array) that projects the entire layer of your design all at once. So instead of drawing 1,000 tiny lines to make one layer, you just project it in a single flash of light. That cuts printing time way down—what takes an hour on an SLA might take 15 minutes on DLP. For a designer cranking out 20 custom engagement ring patterns in a day? That’s a huge win. But wait, don’t write off DLP as just a budget SLA. Jewelry-specific DLP resin is also great for casting, same clean burn as SLA. The only real tradeoff? Detail. Because DLP projects entire layers, the resolution is a tiny bit lower than SLA—think 50 to 150 microns. For most pieces, that’s not even noticeable, but if you’re doing super delicate, micro-sized work, SLA will give you crisper lines. I tell people: if you’re a one-off custom designer making a few pieces a week, DLP is perfect. If you’re doing high-detail filigree or tiny baby jewelry with microscopic engravings, spring for SLA.
Now, there’s a type a lot of people don’t talk about much for jewelry, but it’s been a game-changer for brands that want to skip the casting step entirely: FDM, or Fused Deposition Modeling. Wait, FDM is the one you know from making keychains at home, right? But it’s used for jewelry too, just with a different kind of filament. Most people think FDM is too clunky for fine jewelry, but modern FDM printers use high-temp, low-wax filament specifically made for jewelry. This filament is mostly wax, with a tiny bit of plastic binder, so when you go to cast it, the wax burns out just like an SLA resin—no messy ash. The advantage of FDM here? It’s way cheaper to get started. A good jewelry-focused FDM printer costs a fraction of a SLA or DLP, and the filament is way less expensive per gram than resin. Plus, FDM is super forgiving—you don’t have to deal with messy resin spills, or post-washing pieces. It’s just like loading a spool, hitting print, and walking away. The downside? Detail still lags a bit behind SLA, and layer lines can be visible if you don’t sand them down really well. I’ve seen small shops with FDM printers make solid gold stackable rings that sell for $300 each, no problem, but if they tried to make a delicate lace pendant? The layer lines would show through, and it’d look cheaper than it is. So FDM is great for everyday, simple pieces, not high-end, delicate work.
Then there’s the newest kid on the block, the one that’s actually for making the final metal piece, not just a pattern: Metal 3D Printers. This is where things get wild, because up until now, all the printers I talked about make a pattern that you cast into metal. Metal printers build the metal piece itself, layer by layer, skipping the casting step entirely. How does this work for jewelry? Mostly two types: Powder Bed Fusion (PBF) and Binder Jetting, both used for jewelry. Let’s keep it simple. PBF uses a laser (or an electron beam, for some models) to melt tiny metal powder (gold, silver, platinum) layer by layer, fusing it into a solid piece. Binder Jetting is a bit different: it deposits a liquid binder onto a layer of metal powder to hold it together, then after printing, you bake it to melt the binder and fuse the metal. The big advantage of metal printers? No casting, so you can make really complex designs that are almost impossible to cast. Think interlocking rings with hidden compartments, or a ring with 10 tiny diamond settings that are all perfectly aligned in a weird, asymmetrical shape—casting that would be a nightmare, but a metal printer can do it in a few hours. It’s also way faster for large batches, and you get the final metal piece right out of the printer, no extra steps (other than sanding and polishing, of course). But here’s the catch: metal printers are insanely expensive. We’re talking $50,000 to $200,000, way out of reach for small shops. They also require special facilities—ventilation, fire suppression, because you’re working with molten metal and powder. Only mid-sized to large brands, or high-end custom shops that make ultra-unique pieces, even consider them. I’ve had a handful of clients who bought metal printers to make limited-edition collections, but most still stick to SLA or DLP because the cost is just too high.
Wait, can I mention another type that’s been gaining traction lately, especially for small makers who want to experiment? Low-Resin SLA, sometimes called entry-level SLA printers. These are the $1,000 to $5,000 printers you’ll see on Amazon or jewelry supply websites, way cheaper than industrial SLA. They use the same UV laser and resin, but the build volume is smaller, and the resolution is a bit lower than industrial models. For a hobbyist making custom charms or pendants for friends, or a new designer testing out patterns before buying an industrial machine? These are perfect. I sell a lot of these to new designers who are just starting out, because they can print 5 to 10 pieces a week, test their designs, and if it works, upgrade to a bigger industrial model later. The only downside? They’re not as durable as industrial printers, and you have to replace parts more often, so it’s a tradeoff between cost and longevity.
Now, I know a lot of you are probably thinking: “So which one do I pick?” Let me put this all together in a quick cheat sheet, like I do for my customers. If you’re a hobbyist or a new small designer, testing designs on a budget: go for entry-level SLA or DLP, under $5k. If you’re a mid-sized shop making 10 to 50 custom pieces a week, doing high-detail work: industrial SLA or DLP, $10k to $30k. If you’re making simple, everyday pieces, want to keep costs low: jewelry-specific FDM, under $3k. If you’re a big brand or high-end custom shop making unique, complex pieces, have a big budget: metal 3D printers, $50k+.
Wait, let’s not forget one big thing I always tell people: don’t skip the post-processing. No matter what printer you use, if you cut corners on washing, curing, or sanding, your piece will look like trash. I’ve had clients come to me with a $10k industrial printer, complaining their pieces are turning out bad, and it’s always because they skipped washing the resin off for the casting step, so there’s leftover plastic ash gunking up the mold. It’s simple, but it’s make-or-break.
At the end of the day, the biggest mistake I see people making is buying the most expensive printer they can afford, just because it’s the newest. That metal printer sounds cool, but if you only make 5 pieces a month, you’ll never make back the cost. Take it step by step, figure out what your needs are: what kind of pieces do you make? How many do you make a week? What’s your budget? Once you answer those, picking the right printer is easy.
If you’re curious about testing different types, or want to talk about what would work for your specific jewelry line, feel free to reach out. We’ve helped tons of designers from hobbyists to big brands pick the right equipment, with training and support to make sure you get it right the first time. No pressure, just honest advice.
MJP 3D Printer References:
- Jewelry 3D Printing Market Report, 2024
- Lost Wax Casting Techniques for Modern Designers, 2023
- 3D Printing Technologies for Jewelry, Journal of Jewelry Arts and Manufacturing, 2022
- Small Business Guide to Jewelry 3D Printing, 2023
Hangzhou Originator 3D Technology Co., Ltd.
Hangzhou Originator 3D Technology Co., Ltd. is one of the most experienced jewelry 3d printer manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale high quality jewelry 3d printer made in China here from our factory. Contact us for more details.
Address: Room 403, Building 2, Block B, Heda Incubation Park,No. 452, 6th Avenue, Xiasha, Qiantang District,Hangzhou, Zhejiang, China
E-mail: Sales@originator3d.com
WebSite: https://www.originator3d.com/
